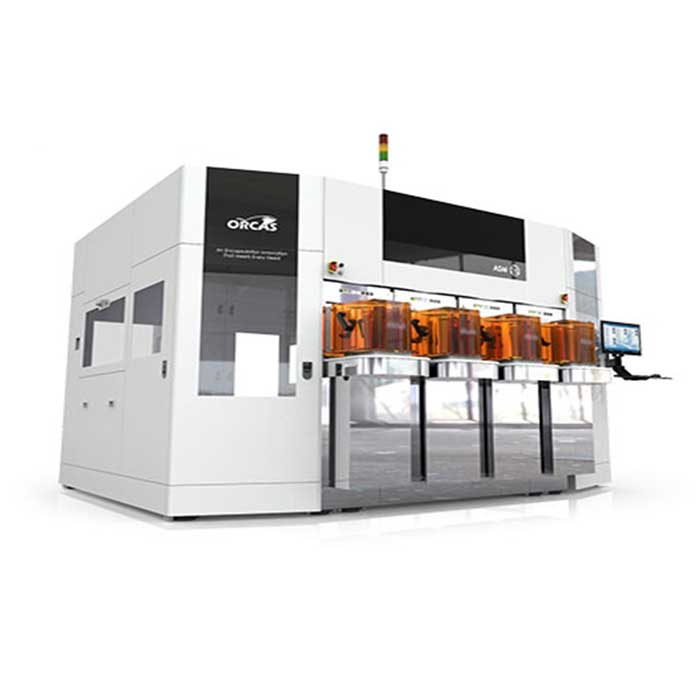
ASMPT ORCAS Semiconductor Molding System
Fan-out/fan-in wafer-level and panel-level packaging — 300mm wafers, 340×340mm panels. Mold direction switchable, liquid...
We stock used molding systems from TOWA, Besi Fico, ASMPT, APIC YAMADA and other platforms — transfer molding, compression molding and C-Molding systems for leadframe, substrate, wafer and panel packaging. The machine that fits your line depends on four things: the package format, the molding method, the resin system and the production volume. Most used-molding-machine purchases that go wrong fail at one of these four points — the model matches, the machine arrives, and then the mold chase or tooling turns out not to fit the target package. Tell us your requirements and we'll shortlist the systems that actually work on your line.
We've seen buyers order a molding machine based on the model number alone, then discover the mold chase doesn't fit their leadframe strip — and finding a replacement chase for a discontinued platform can take months. The same molding platform is not automatically suitable for every semiconductor package. Leadframe products, substrate-based arrays, power modules, wafers and panels place different demands on mold size, clamp force, resin delivery, release film, handling and post-mold cleaning.
Tell us what is entering the mold and what the finished package should look like. This is usually more useful than starting with machine tonnage alone.
QFN, SOP, DIP, discrete and related molded packages.
Leadframe size, cavity layout, pellet delivery, wire-sweep risk, chase and tooling compatibility.
BGA, MAP-QFN, SiP and multi-die package arrays.
Substrate dimensions, mold thickness, resin flow length, exposed features and singulation route.
FOWLP, FIWLP, EWLP, PLP and advanced package structures.
Wafer or panel size, dispense pattern, resin form, thickness uniformity, release film and warpage control.
Thick devices, heat-spreader exposure, modules, sensors and LED-related products.
Device height, thermal path, exposed metal, liquid or granular resin, mold pressure and demolding method.
Two molding machines with the same model name can have very different capabilities. The installed press, mold interface, handling modules, software and included tooling matter more than the platform name alone. Review the current inventory, then send us your package and mold requirements for a configuration check.
Fan-out/fan-in wafer-level and panel-level packaging — 300mm wafers, 340×340mm panels. Mold direction switchable, liquid...
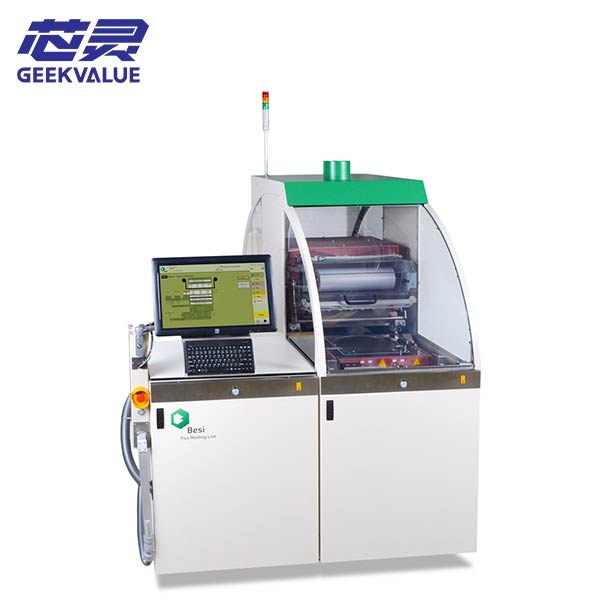
Besi Fico FML molds wafers and panels. Up to 305mm wafers, 300×340mm panels. Overmolded and exposed die both run in the ...
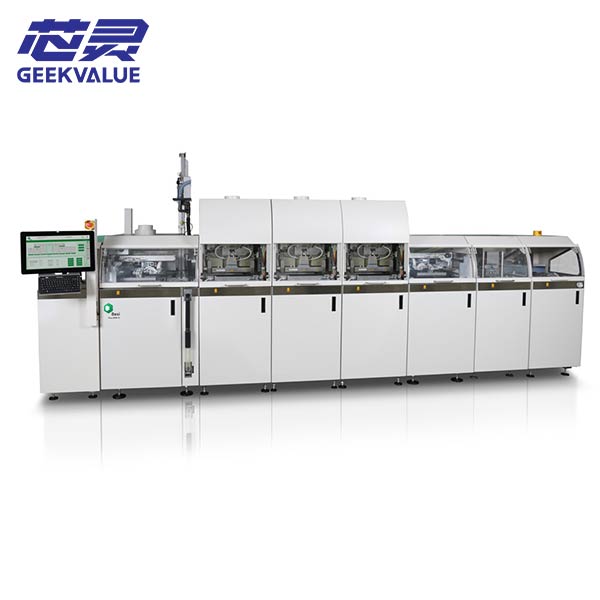
Besi AMS-X leadframe molding system, up to 240 leadframes/hour, about 30% faster than comparable tools. Four independent...
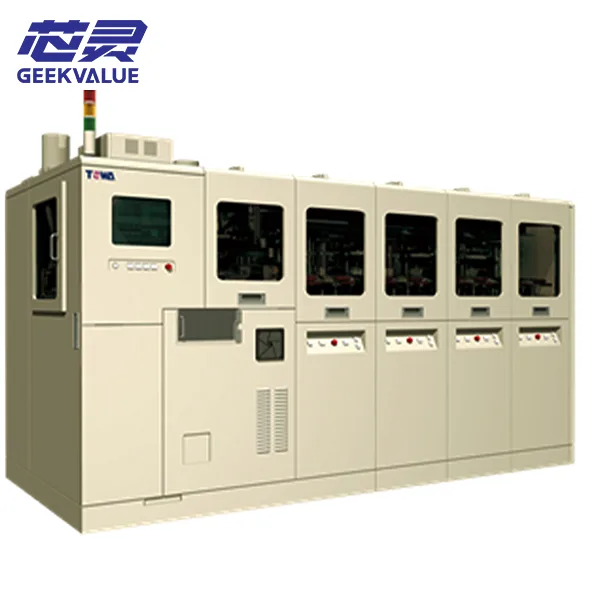
TOWA Y1E4120 transfer molding system. 120-ton clamp force, frames up to 78 × 260 mm. Modular design — add or remove pres...
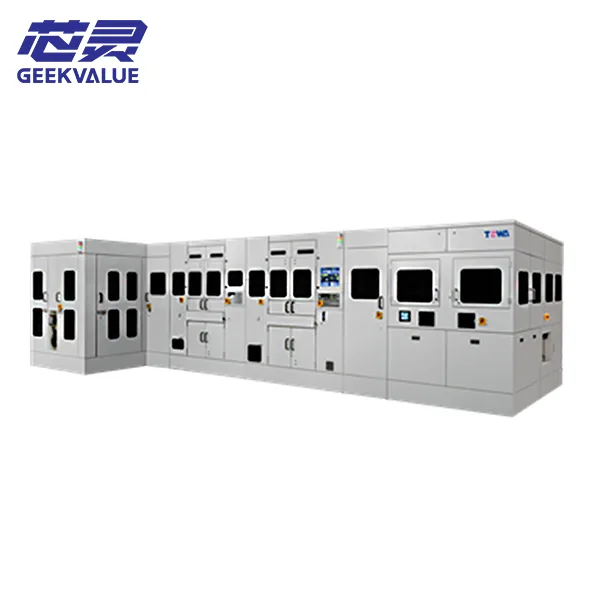
TOWA CPM1180 large-panel compression molding. Handles up to 660×620mm panels and 18" (Φ450mm) wafers. Cavity-down d...
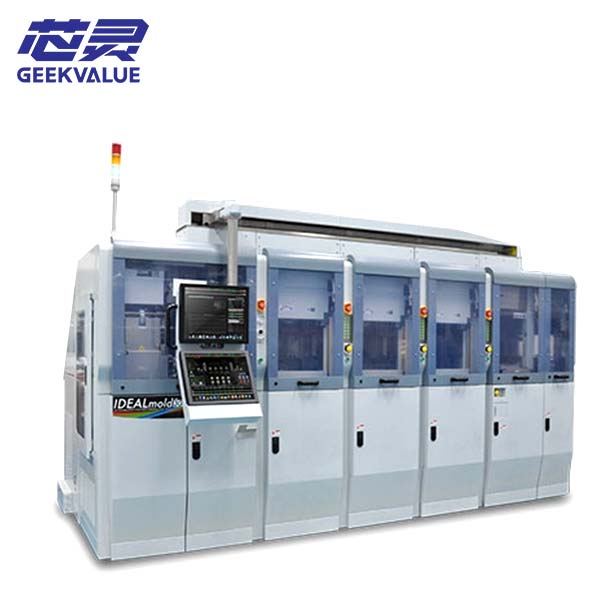
The ASMPT IDEALmold 3G molds strip and reel substrates, leadframes up to 100 × 300 mm. Start with one press, scale to fo...
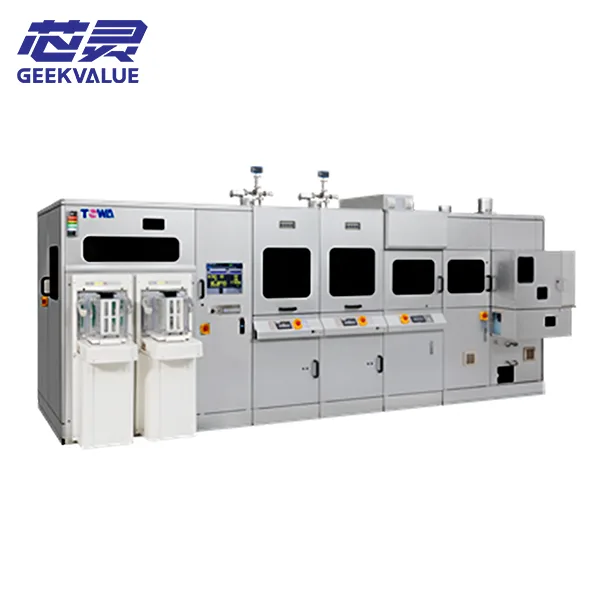
The TOWA CPM1080 WLP/PLP compression molding system supports both granular and liquid resins and is compatible with 300m...
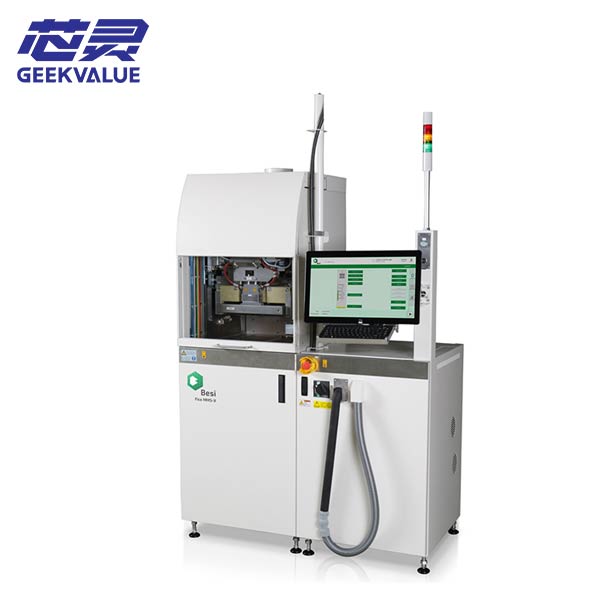
Besi MMS-X is the manual version of the AMS-X molding system. Strips up to 125 × 300 × 10 mm, 180-ton clamp force, 150 m...
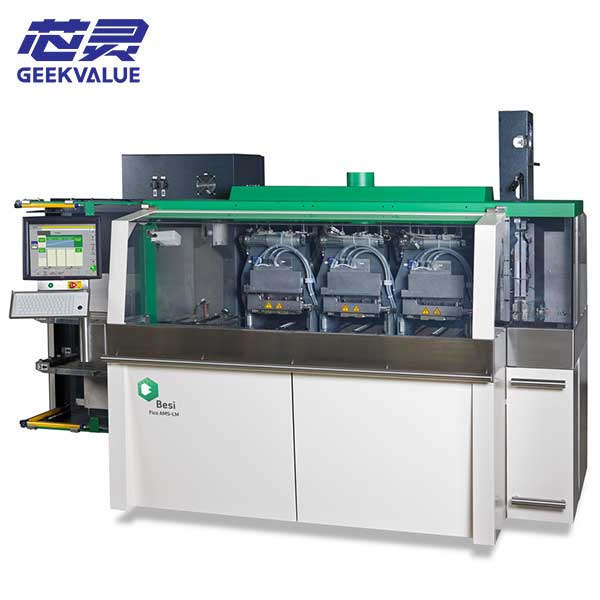
Besi Fico AMS-LM large-substrate molding system, strips up to 102 × 280 mm. Mk3 handles SIP, dual-side, MEMS. 600 kN cla...
Pre-owned ASMPT IDEALmold R2R semiconductor molding system. Ask about line configuration, mold compatibility, machine co...
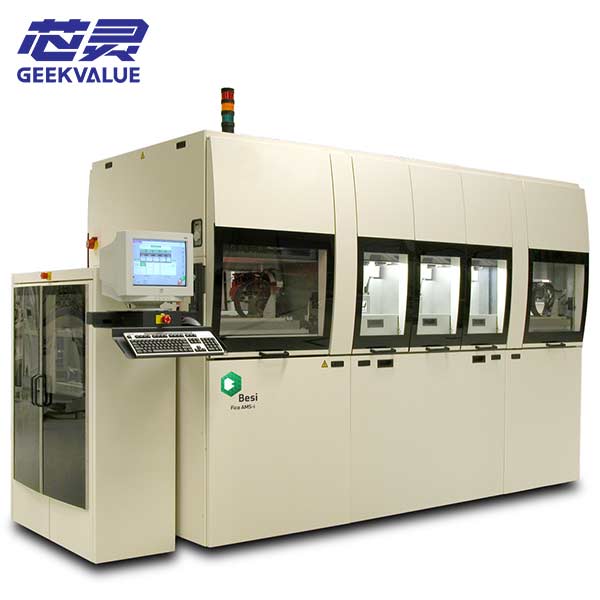
Pre-owned Besi Fico AMS-i automatic molding system for semiconductor packages. Ask about configuration, molds, condition...
The difference is mainly how the resin reaches the package. This affects resin movement around the device, mold construction, material use, package size and the type of product the machine is designed to handle. T-Molding still holds the majority of global revenue for mature packages, while C-Molding is gaining share in FOWLP, FOPLP and MUF applications.
The mold closes first, then heated resin is transferred through runners and gates into the package cavities before curing.
Resin is dispensed or placed into the mold area and compressed around the device, reducing the need for long transfer paths.
We've seen buyers focus on press force during machine selection, then discover the vacuum system can't evacuate the mold fast enough and the package ends up with voids. Output is not determined by press force alone. Resin behavior, mold temperature, vacuum, clamp balance, package layout, wire geometry, release condition and post-mold handling all affect the finished package.
When replacing an existing molding machine, share current defects and package samples. They often reveal more than a general request for a “higher-capacity” system.
Resin flow can move long or closely spaced bond wires during encapsulation.
Air removal, vacuum, preheat, resin condition and feature geometry influence filling.
Mold contact, clamp balance, film, chase condition and process pressure affect overflow.
Large substrates, wafers and panels require controlled pressure and resin distribution.
Release film, mold surface, cure condition and eject sequence affect package removal.
Manual, modular and fully automatic molding systems serve different production environments. The right choice depends on package changeover, loading format, mold exchange, resin handling, traceability and the volume expected from each product family.
Useful for process development, package trials, low-volume production and applications where operators load the package, resin and tooling directly.
Combines controlled molding with selected automation for loading, preheating, resin handling or unloading.
Designed for repeatable high-volume encapsulation with automated loading, resin management, molding, unloading and production data handling.
We've seen buyers purchase a used molding machine based on a model number, then discover the hydraulic system needs a full rebuild or the heater zones are out of spec — issues that cost more than the initial savings. A used semiconductor molding machine may have been configured for one package family, resin system or factory layout. Before quotation, the installed press, mold interface, handling units, software, utilities and included accessories should be reviewed as one system.
Start with the package, resin and production route. A model can then be checked against the actual mold, handling and process configuration required.
It encapsulates semiconductor chips, interconnects and package structures with cured resin to provide mechanical protection, environmental isolation and the final molded package form.
Transfer molding moves heated resin through runners and gates into a closed mold. Compression molding places or dispenses resin in the mold area and compresses it around the device. The suitable method depends on package architecture, resin flow requirements and production format.
No. Compatibility depends on mold dimensions, clamp force, resin delivery, chase and tooling, package handling, software and the options installed on the actual machine.
Compression molding is widely considered for many wafer- and panel-level applications, but the final choice still depends on wafer or panel size, resin form, dispense method, target thickness, release-film handling and warpage limits.
Wire sweep can result from resin flow acting on bond wires. Wire length, loop geometry, package layout, flow path, viscosity, fill speed, temperature and mold design all influence the risk.
Confirm the exact model, year, molding method, press and mold interface, handling modules, software, vacuum and heating systems, included tooling, maintenance history, operating condition, utilities and refurbishment scope.
Send the target package, strip or wafer size, molding method if known, resin type, mold dimensions, output requirement, preferred manufacturer or model, required condition, quantity and destination country.
Send the package format, resin, molding method, mold or chase information, output requirement and preferred machine condition. We'll confirm availability, mold compatibility and configuration completeness within 4 business hours.